menu

Zibo Horizon Environmental Technology Co., Ltd.,
(Export Office: Zibo Joyreach New Materials Co.,Ltd).
Our company has been a leading brand of medical water purification in China since 2012.We combine R&D,design,production,sales,and service to deliver high-quality water treatment solutions for the medical and healthcare industry.
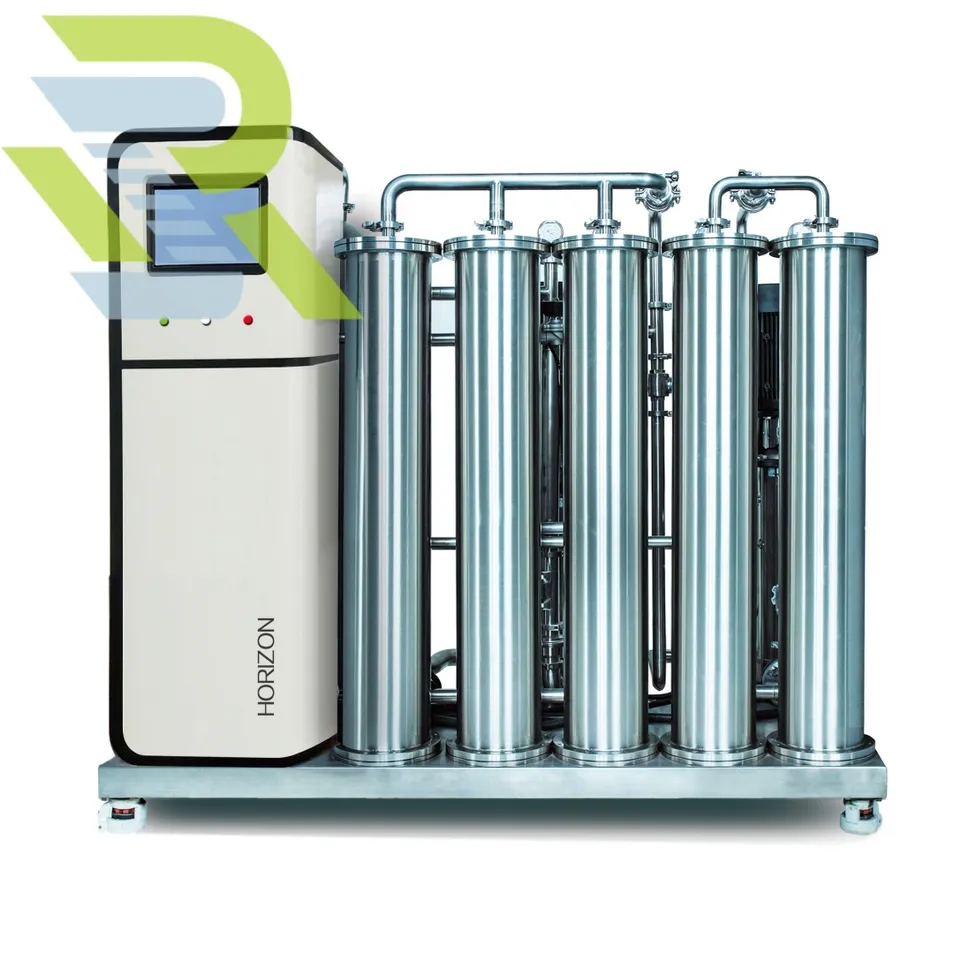
HHHD Hematodialysis(Hemodialysis) Water Treatment System For Hospital HD Department.
The HHHD-RO water treatment equipment is specifically designed for hemodialysis rooms and centers,meeting the stringent water quality requirements essential for safe and effective hemodialysis treatment.This advanced system is fully compatible with a wide range of domestic and international dialysis machines,ensuring seamless integration into any dialysis facility.By delivering consistently high-purity water,the HHHD-RO series provides a reliable and efficient foundation for optimal dialysis therapy.For Hemodialysis department,we focus on it's water purification system for many years.
FAQ:
Before providing a quotation for the water treatment machine, we need to know the following information:
1- The quality of the feed water: water test report.
2- The quality of finished the purified water: such as chemical content and conductivity. We have it's standard water report for HD dept, you could share yours.
3- The production capacity of HD RO pure water (L/H) OR you can tell us how many beds need to use RO water.
Such as every 3 beds need 100LPH, every 7 beds need 300LPH, every 15 beds need 600LPH and every 20 beds need 1000LPH,we can make suggest according to beds qty.
4- A layout drawing of the installation room(s).
5- It has High-temperature heat disinfection and Chemical disinfection.
Which method does your side need? Normally, Heat disinfection is expensive than Chemical disinfection.
>>>Generalization:
1. Comply with YY0572-2015 and YY0793-2010 hemodialysis water quality standards;
2. Meet the AAMI/ASAIO standard for hemodialysis water in the United States;
3. Meet the relevant requirements of Standard Operating Procedures for Blood Purification (2010);
4. Ion removal rate:≥ 99.5%;
5. Bacterial endotoxin removal rate: ≥ 99.9%;
6. Water quality:total bacterial count ≤ 10CFU/ml;
7. Water quality:endotoxin<0.03EU/ml.SpecificationTechnical Specifications>>>Models HHHD-RO
| Model | Water Output L/H(25℃) | Power(K w) | Supply For Beds' Qty (Set) | Weight (Kg) | Dimension (L×W×H)Mm |
| HHHD-RO | 300 | 380V/4.0 | 3-7 | 260 | 900x750x1600 |
| 600 | 380V/5.0 | 5-15 | 300 | 1500x750x1750 | |
| 1000 | 380V/7.0 | 10-25 | 400 | 1500x750x1750 | |
| HHHD-RO | 1200 | 380V/10.0 | 15-30 | 480 | 1200x750x1750 |
| 1500 | 380V/10.0 | 20-40 | 550 | 1200x750x1750 | |
| HHHD-RO | 2000 | 380V/12.0 | 30-70 | 650 | 1500x750x1750 |
| 3000 | 380V/12.0 | 40-80 | 750 | 1500x800x1750 |
>>>The HHHD-RO Water Treatment System Consists of:
1. Automatic Pretreatment System:
Comprising a raw water booster pump,pre-filter,multimedia filter,activated carbon filter,water softener,and a final precision filter to ensure feed water quality for the downstream RO process.
2. Reverse Osmosis Host:
Featuring a two-stage RO design for high-purity water production,a concentrate water recycling system to enhance water efficiency,and an integrated automatic control system for reliable operation.
3. Water Supply & Distribution Loop:
Engineered with a U-type main circulation loop and a U-type secondary circulation loop to maintain constant flow velocity and prevent bacterial growth,ensuring water purity at the point of use.
4. Automatic Disinfection System (Optional):
4.1 Chemical Disinfection System
4.2 Pasteurization (90°C) and Over-temperature (121°C) Sterilization System
5.Remote Monitoring System:
Enables real-time remote supervision of various operating parameters and equipment working status via mobile phone or computer,facilitating proactive system management and maintenance.
>>>Technical Design Features:
1. Advanced Bacteria Control
1.1 Zero Dead-Leg Design:The system is engineered with 3D principle technology to eliminate dead legs and prevent water stagnation.
1.2 Turbulent Flow Prevention:U-type main + secondary circulation ensures flow velocity >1 m/s,creating turbulent flow that inhibits bacterial growth and attachment.
1.3 Non-Dead Chamber Housings:Special membrane housing design ensures complete water flow and no residue during disinfection.
2. Advanced Endotoxin Control
2.1 Ultra-pure dialysis technology ensures high-efficiency endotoxin removal.
2.2 Production water washing process minimizes bacterial endotoxin growth.
3. Reliable Disinfection Technology
3.1 Heated disinfection process with tankless,zero dead-leg design reduces bacteria breeding.
3.2 Online integrated non-contact heating ensures efficient disinfection,cleaner water quality,and safe water-electricity isolation.
4. Stable and Reliable Rlectrical Design and Operation Mode:
4.1 Simple and practical operation interface,stable and safe control system;
4.2 Two-stage reverse osmosis is directly coupled,and the produced water is directly supplied to the dialysis machine through circulation,and there is no produced water tank for storage;
4.3 The whole system is designed with no dead space,and operates with automatic pulse washing day and night to prevent the growth and attachment of microorganisms;
4.4 It has the functions of thermal disinfection and chemical disinfection,and can realize full-automatic one-button disinfection;
4.5 Multiple working modes operate independently,with 1-RO, 2-RO and two levels to fully ensure the safety and continuity of dialysis;
4.6 Real-time monitoring of conductivity,temperature,pressure and other operating parameters,with multiple alarm safety protection functions.